
Introduction
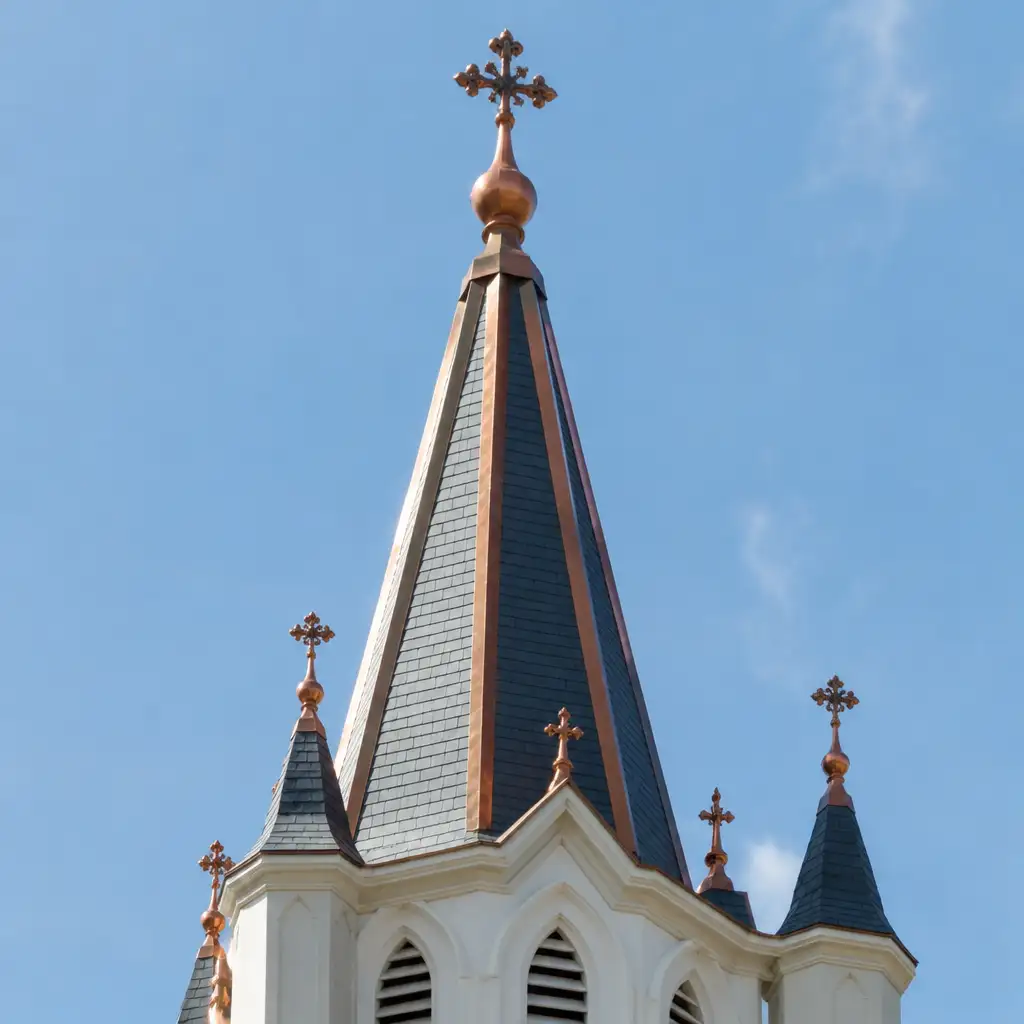
Preservation contractors and architectural metal trades in Southeastern Massachusetts regularly encounter historic rooftops, cupolas, and steeples where copper finials and ornamental components are either missing or beyond repair. Reproducing these elements requires a practical balance of measured drawing discipline, fabrication tolerances, and repair techniques that respect the original construction while meeting modern durability expectations. This article focuses on copper finials and provides guidance tailored to restoration projects in Massachusetts and New England.
The guidance below is written for roofing contractors, preservation specialists, and architectural metal fabricators who supply or install custom copper ornamentation. It emphasizes on-site documentation, realistic tolerance bands for shop fabrication, appropriate welding and soldering approaches, and strategies for matching historic patinas so replacements read correctly on aged structures.
Sections cover measured-drawing workflows, recommended fabrication tolerances for visible and structural interfaces, common one-off reproduction challenges, mounting reinforcement strategies, repair-welding and soldering tips, and patina-matching techniques. Where relevant, the guidance references related product categories and procurement pathways familiar to trade professionals.
Throughout, the focus remains technical and contractor-oriented: how to document, specify, and execute copper finial reproductions that integrate with existing roof systems and stand up to coastal New England conditions.
- Introduction
- Measured-Drawing and Template Workflows
- Specifying Fabrication Tolerances for Copper Finials
- Fabrication Methods: Spinning, Forming, and One-Off Techniques
- Mounting Reinforcement and Connection Details
- Repair Techniques: Soldering, Brazing, and Welding Best Practices
- Patina Matching and Surface Finish Strategies
- Frequently Asked Questions
Measured-Drawing and Template Workflows
Accurate measured drawings are the foundation of any successful reproduction. Start on-site with a controlled measurement strategy: identify datum points, establish primary control lines relative to roof ridges or cornices, and record multiple cross-sections of the finial base and attachment area. For complex three-dimensional forms, capture photographs from orthogonal directions and include scale references in each shot.
Field templates remain invaluable for one-off finials. Produce full-size paper or thin plywood templates of profiles and base diameters. Templates allow quick verification of clearances with surrounding roof features and ensure the shop can replicate exact mating surfaces. For highly irregular or deteriorated originals, consider 3D scanning or photogrammetry to capture subtle geometry, then convert scans into shop drawings or CNC patterns.
Shop drawings should include plan, elevation, and a section through the mounting interface with dimensions and tolerance callouts. Specify material thickness, suggested seams, internal stiffeners, and any hidden reinforcement. For trade-only fabrication needs or examples of historical ornament types, review existing product references for guidance such as the leader boxes and finials catalog available from trusted fabricators.
Specifying Fabrication Tolerances for Copper Finials
Tolerances for reproduced copper finials should be realistic and tied to function and visibility. For visible ornamental surfaces and mating features that affect aesthetics, hold tighter tolerances — typically ±1/16″ to ±1/8″ — to avoid glaring misalignments at sightlines. For structural interfaces such as base plates and internal brackets, tolerances of ±1/8″ to ±3/16″ are acceptable provided the connection details allow field adjustment.
When dimensioning shop drawings, call out tolerances separately for three areas: visible seams and ornamental geometry, mating/mounting interfaces, and internal reinforcement. Example: ornamental profile ±1/16″, skirt diameter ±1/8″, mounting bolt pattern ±3/16″. These bands allow the shop to form details accurately while permitting onsite alignment by the installation crew.
Specify material thickness based on historic evidence and current performance requirements. Common choices are 16 oz or 20 oz copper for finials; thicker 24 oz may be used for larger or structural pieces. Thickness affects forming springback and the achievable tolerances—document the exact gauge in the drawings so the fabricator can compensate during forming and seaming operations.
Fabrication Methods: Spinning, Forming, and One-Off Techniques
Selecting the appropriate fabrication method depends on the finial geometry, quantity, and required finish. Spinning works well for rotationally symmetric finials and produces smooth, continuous surfaces suited for historic shapes. Hand-forming and dolling are preferred for complex profiles with sharp transitions or for pieces requiring an exact match to an extant example.
Machine forming and CNC-assisted patterning can produce repeatable parts when a set of reproductions is required. For true one-off reproductions, traditional patternmaking—creating a physical plug, wax or wooden master, and then forming a copper skin over a mold—remains the most reliable way to match idiosyncratic historical details.
When choosing seams and closures, specify the seam type on drawings: standing seams, folded hems, or soldered lap seams. Each has different tolerance implications. Discuss with the fabricator whether seams should be concealed or exposed, and plan for seam reinforcement if the finial will be climbed on or receive wind loading consistent with coastal Massachusetts conditions.
Mounting Reinforcement and Connection Details
Mounting systems must transfer wind and uplift loads into the structure without concentrating stresses at the copper. Typical reinforcement strategies include internal stainless-steel spines or a solid stainless shank welded or mechanically fastened to a backing plate. Use 316 stainless steel for fasteners and reinforcement in coastal environments to resist corrosion.
Design the base plate and anchorage to accept field-adjustable connections. Oversized holes for leveling bolts, slotted plates, or captive shims permit installers to align finials precisely without overworking the copper. Seal penetrations with compatible roof sealants and provide a sacrificial flashing detail that isolates the copper from dissimilar metals and masonry mortar.
Integrate the finial base with adjacent flashing and roof details to maintain weather-tightness. Coordinate with the roofing scope and refer to copper roofing and flashing details when necessary; related product guidance and examples for roof panel integration can be found in resources for roofing panels and flashings. Always document the sequence for installing the reinforcement and flashing so field crews can execute without compromising the roof membrane.
Repair Techniques: Soldering, Brazing, and Welding Best Practices
Repair of historic copper finials requires selecting the method that preserves as much original material as possible while restoring structural integrity. For seam repairs and small tears, soft soldering with modern lead-free solders is appropriate for non-structural joints. Use a quality copper flux designed for soft solders and avoid overheating which can anneal thin copper and soften formed details.
When repairs must carry load — for example when reattaching a base shank or reconstructing a damaged collar — brazing or TIG welding with a suitable copper filler provides stronger joints. Brazing with silver-based or copper-phosphorus alloys can be effective where aesthetics require a narrow heat-affected zone. TIG welding is a specialized skill on copper; it requires experienced operators and often pre-heating for thick sections to avoid cracking.
Mechanical reinforcement combined with solder or brazed closures is often the most durable approach. Install internal stainless-steel plates, rivets, or tabs to bridge damaged areas, then dress the outer surface with solder or braze. For historic-sensitive projects, document repair methods and materials so future custodians understand the interventions and so the work remains reversible where possible.
Patina Matching and Surface Finish Strategies
Matching a historic patina is central to visual continuity. Patinas on New England buildings vary from warm browns to blue-greens depending on exposure, pollution, and age. The most reliable strategy is to create small test panels fabricated to the same thickness and forming method, then age or chemically treat them until they approximate the surrounding copper.
Chemical patination can accelerate natural color development but must be tested because reactions are sensitive to existing substrate conditions, previous coatings, and nearby materials. Controlled application of patination solutions on shop samples allows approval by the preservation team before treating the actual finial. Avoid irreversible surface treatments unless they are specified and accepted by the owner and architect.
For continuity at the jobsite, consider blending new copper to adjoining surfaces by partially pre-patinating and then allowing natural weathering to complete the match. When matching to extensively weathered elements, consult with the project team about whether to install a protective coating or let the piece age naturally; each choice has maintenance and visual trade-offs over time.
Frequently Asked Questions
Q: What fabrication tolerance should I require for a one-off decorative copper finial?
A: Specify tight visual tolerances of ±1/16″ to ±1/8″ for ornamental profiles and ±1/8″ to ±3/16″ for mounting interfaces. Call out tolerances separately on shop drawings so the fabricator can prioritize visible alignment versus structural fit.
Q: Can damaged copper finials be welded or should they be replaced?
A: Small tears and non-structural seam failures are often repairable with soft soldering. Structural repairs typically require brazing or TIG welding plus internal stainless reinforcement. The decision depends on remaining material condition and historic significance; document repairs for future reference.
Q: How do I get a new finial to visually match adjacent aged copper?
A: Fabricate shop test panels and trial patinate them to match the existing range. Use a combination of pre-patination, approved chemical treatments, and controlled field blending. Always test before applying treatments to the finished component.
Working from drawings, field measurements, or a custom detail? Cape Cod Copper partners with trade professionals to fabricate copper components made to fit the job, from custom flashings and roof panels to leader heads, chimney caps, vents, and decorative architectural details. Call (508) 946-1999 or email capecodcopper2@gmail.com to review your project requirements.